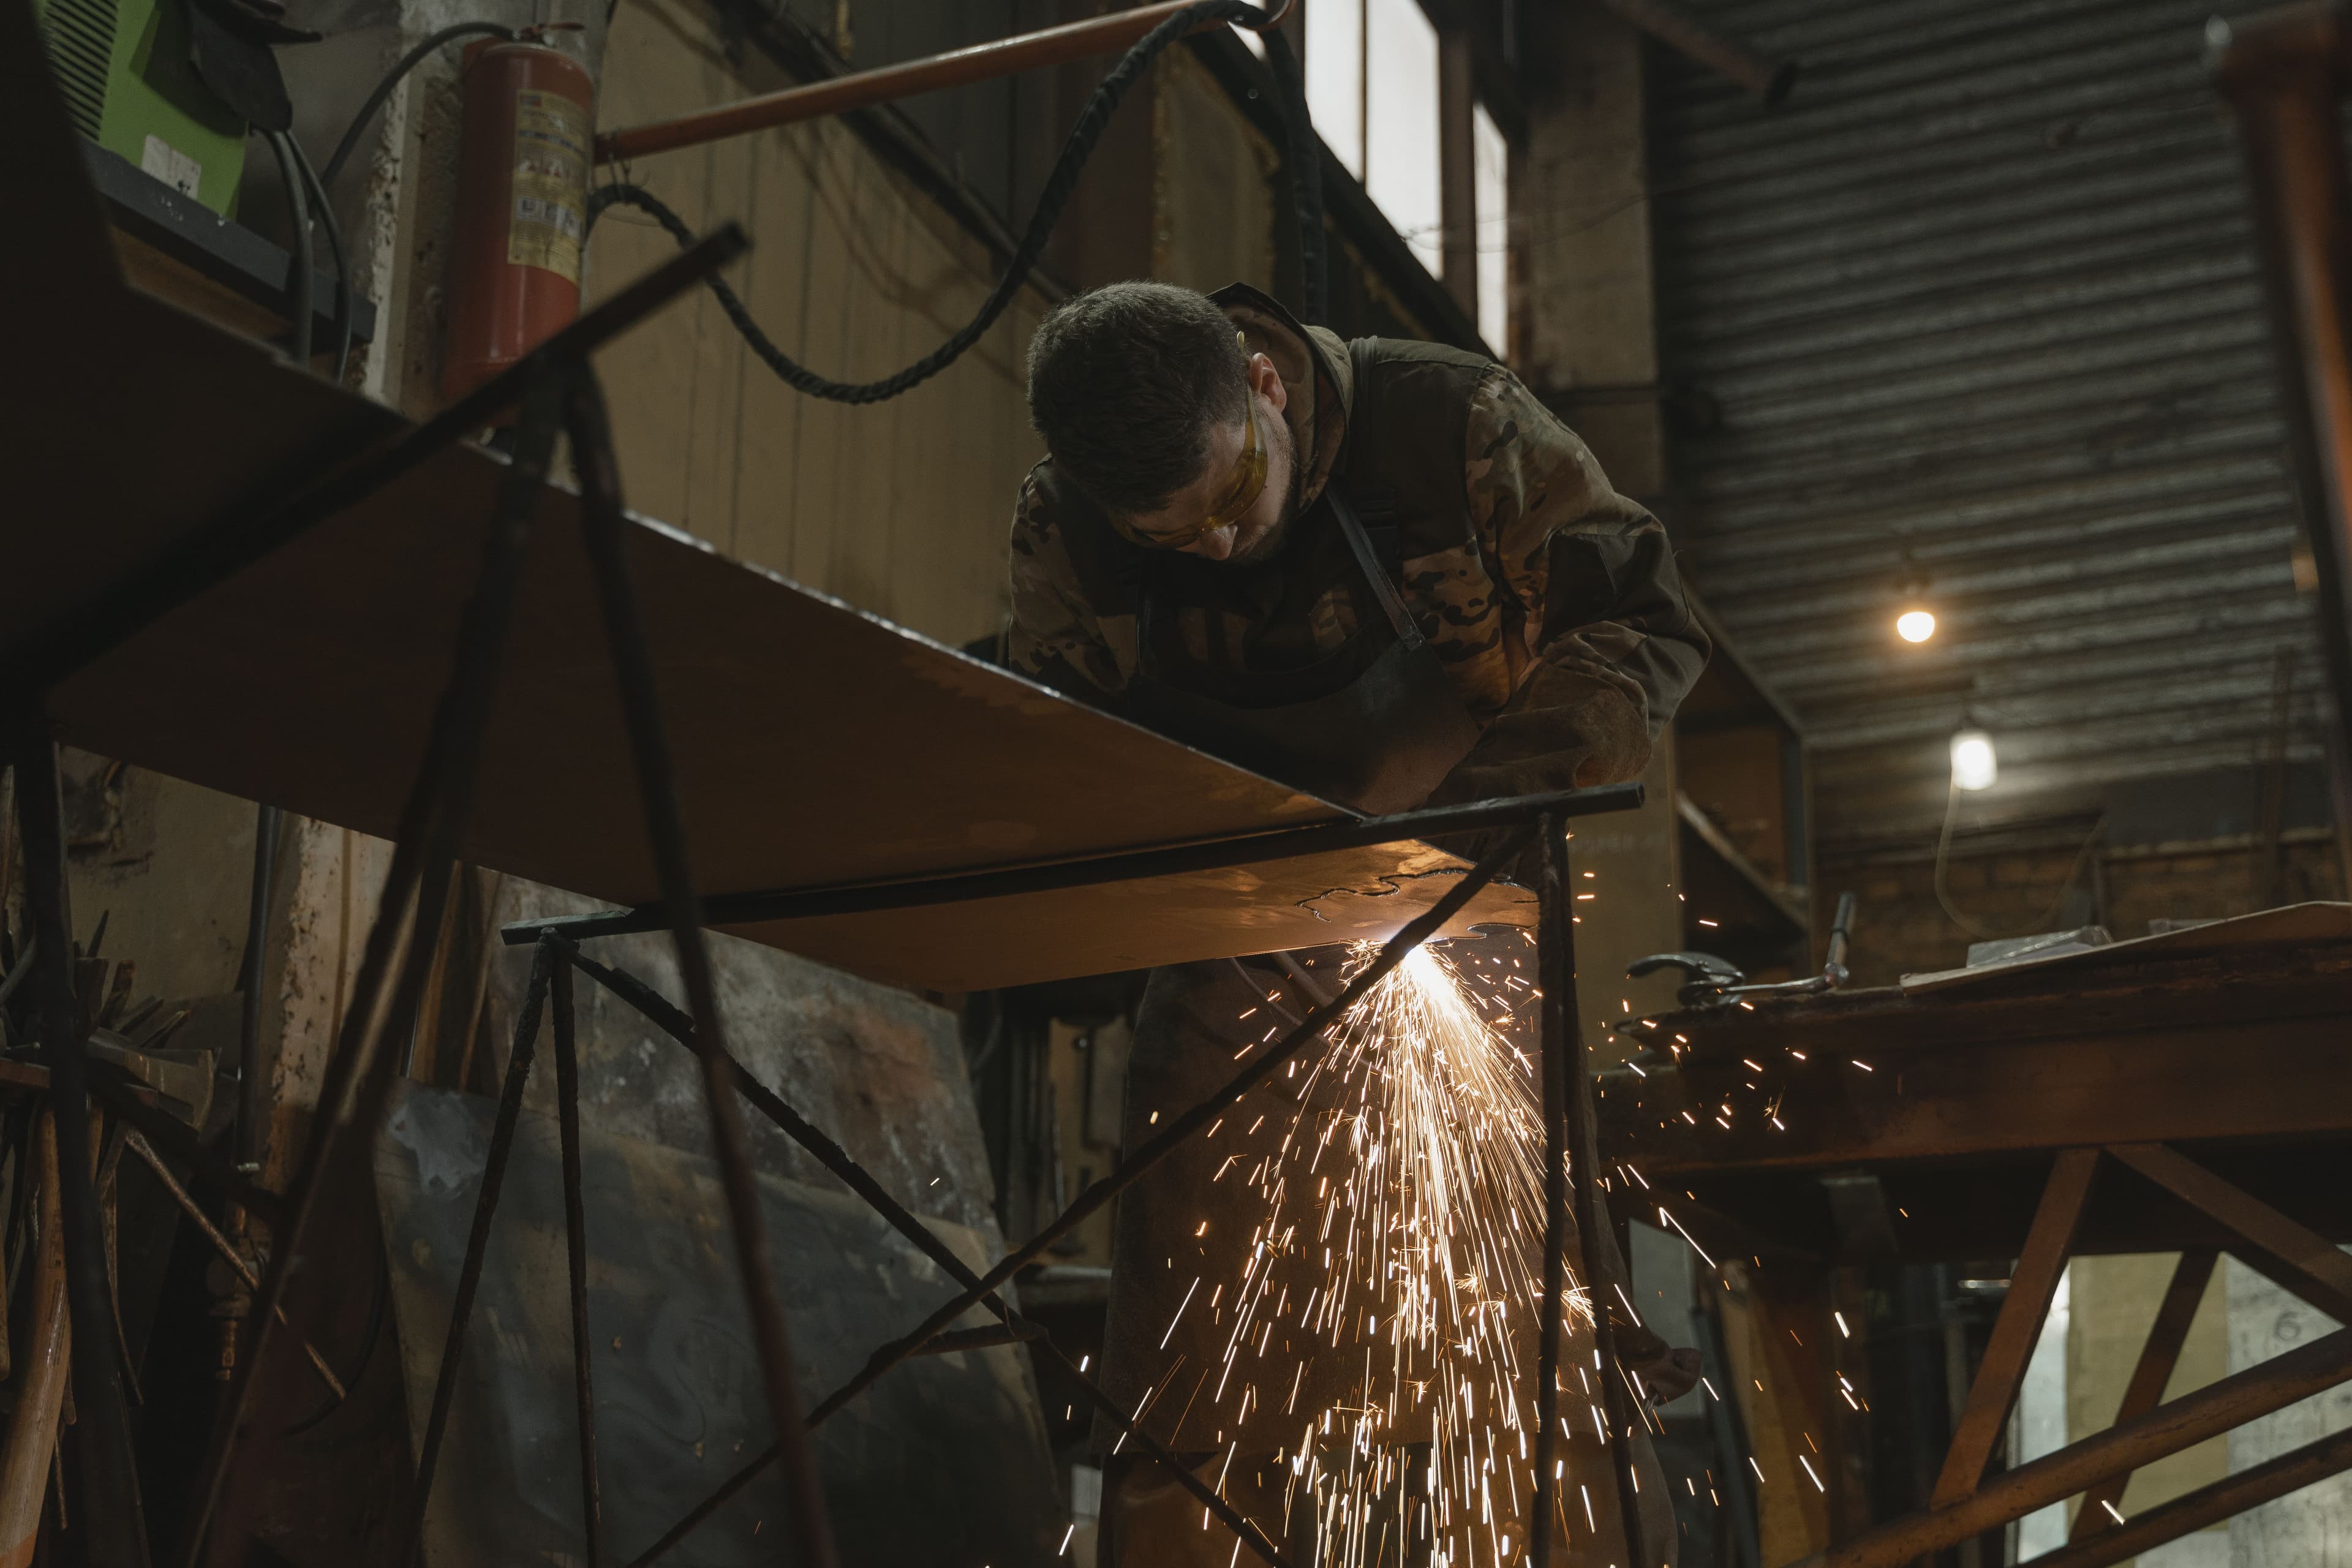
CNC Machining Tolerances: ISO 2768, GD&T, and Cost Trade-Offs
Content in this Article
CNC Machining can look straightforward in CAD and still fail after printing, finishing or inspection. The useful question is not whether a process can make the geometry once, but whether the chosen material, orientation and acceptance method can deliver the required function repeatedly. This guide turns that decision into a practical review workflow.
- Define the operating environment, functional load, quantity and acceptance criteria before choosing a process.
- Treat dimensions and performance values as design-starting points; confirm the exact grade and supplier capability before release.
- Use a first article or pilot lot to lock inspection and process controls before scaling.
Start with requirements and process selection
ISO 2768 General Tolerance Classes
ISO 2768-1 covers linear and angular dimensions without individual tolerance indication. Choosing the right class as a default keeps your drawing readable and your shop happy.
| Nominal size (mm) | f (fine) | m (medium) | c (coarse) | v (very coarse) |
|---|---|---|---|---|
| 0.5–3 | ±0.05 | ±0.10 | ±0.20 | — |
| 3–6 | ±0.05 | ±0.10 | ±0.30 | ±0.50 |
| 6–30 | ±0.10 | ±0.20 | ±0.50 | ±1.00 |
| 30–120 | ±0.15 | ±0.30 | ±0.80 | ±1.50 |
關鍵設計動作: Set the title block to 2768-m by default. Reserve 2768-f or individual tighter callouts for fits, datums, and sealing surfaces — anything else inflates inspection time without functional return.
CNC Machining: define requirements before selecting a process
Connect requirements, process decisions and inspection before the first build to reduce late design changes.
- 1Requirements
Function, service environment, quantity and failure risk
- 2Material and process
Material grade, build strategy, geometry and finishing
- 3Inspection
Critical dimensions, functional tests and lot records
Key design rules
Cost Multipliers vs Tolerance Class
| Class | Example | Cost multiplier | Driver |
|---|---|---|---|
| Coarse (2768-c) | ±0.20 mm / 30–120 | 1.0× | Single op, minimal QC |
| Medium (2768-m) | ±0.10 mm / 30–120 | 1.3× | Default tooling, sample QC |
| Fine (2768-f) | ±0.05 mm / 30–120 | 2.0× | Tool comp, full inspection |
| Precision | ±0.013 mm | 4–6× | Grinding/EDM, climate room |
Material Effects on Achievable Tolerance
Plastics drift after machining; let parts soak at inspection temperature for several hours before CMM. Titanium springs back after heavy cuts; finish passes need light depth and sharp geometry.
From prototyping and finishing to acceptance
Tolerance Stack-Up and GD&T Basics
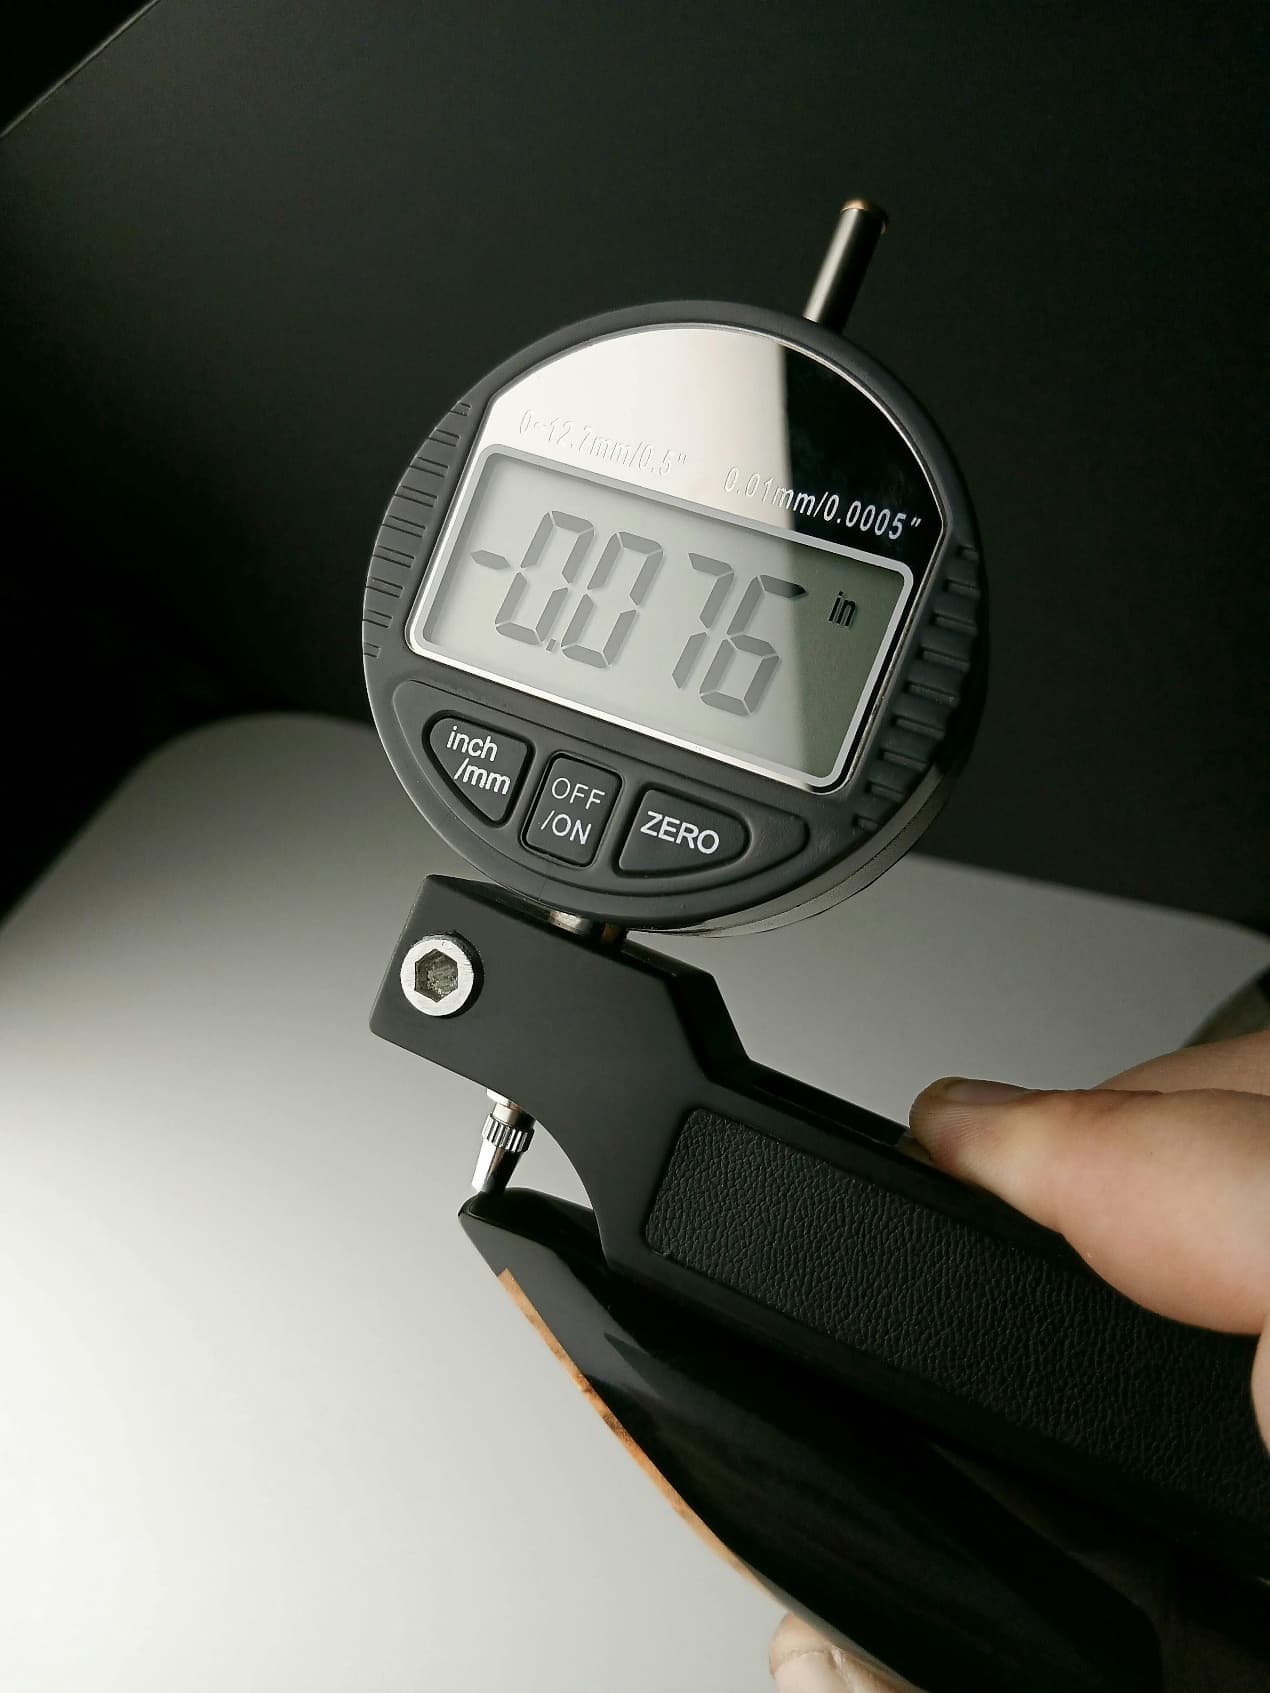
A simple ±0. 05 mm on three stacked features can accumulate to ±0.
CNC Machining: four checks before RFQ
- Function
State what the part must do and where it will be used
- Material and process
Name the required grade or performance range
- Design controls
Mark critical geometry, orientation and finishing
- Acceptance
Define dimensions, tests and required records
Pre-RFQ review: recommended practice and common mistakes
| Recommended practice | Common mistake |
|---|---|
| Default the title block to ISO 2768-m | Apply ±0.025 mm globally |
| Tighten only functional features | Tighten cosmetic edges and chamfers |
| Specify GD&T with clear datums | Mix linear and GD&T on the same feature |
| Declare surface finish where it matters | Leave Ra unspecified on sealing faces |
- Title block default class set (recommend ISO 2768-m)
- All tight tolerances justified by a function note
- Datum reference frame defined on every GD&T callout
- Surface finish (Ra) specified on sealing, sliding, and cosmetic faces
- Stack-up analyzed (worst-case + RSS) for mating features
FAQ, further reading and sources
What should you define first for CNC Machining?
Define the operating environment, functional load, quantity and acceptance criteria before choosing a process. Those requirements determine the material, design rules and inspection plan.
Can the typical values in this guide be released directly on a drawing?
No. Use them for early design, then confirm the exact grade, supplier capability, DFM response and first-article result.
What should be locked before scaling production?
Lock the material, process settings, orientation, finishing and inspection method. Confirm that different lots reproduce the first-article result before scaling.
Next, explore 3D printing services, materials, online quoting, and the related design guides linked below.