Combining Part Assemblies With Additive Manufacturing
Content in this Article
Part Consolidation creates value when geometry, volume, revision frequency and functional requirements fit additive manufacturing. This guide connects process, material, design and inspection decisions.
- Define function, environment, quantity and risk before selecting a material or process.
- Treat typical values as comparison points; confirm the exact grade and supplier capability before release.
- Use a first article or pilot lot to verify dimensions, function and records before scaling.
Define the decision
Document function, environment, quantity and risk so every option is compared against the same requirement.
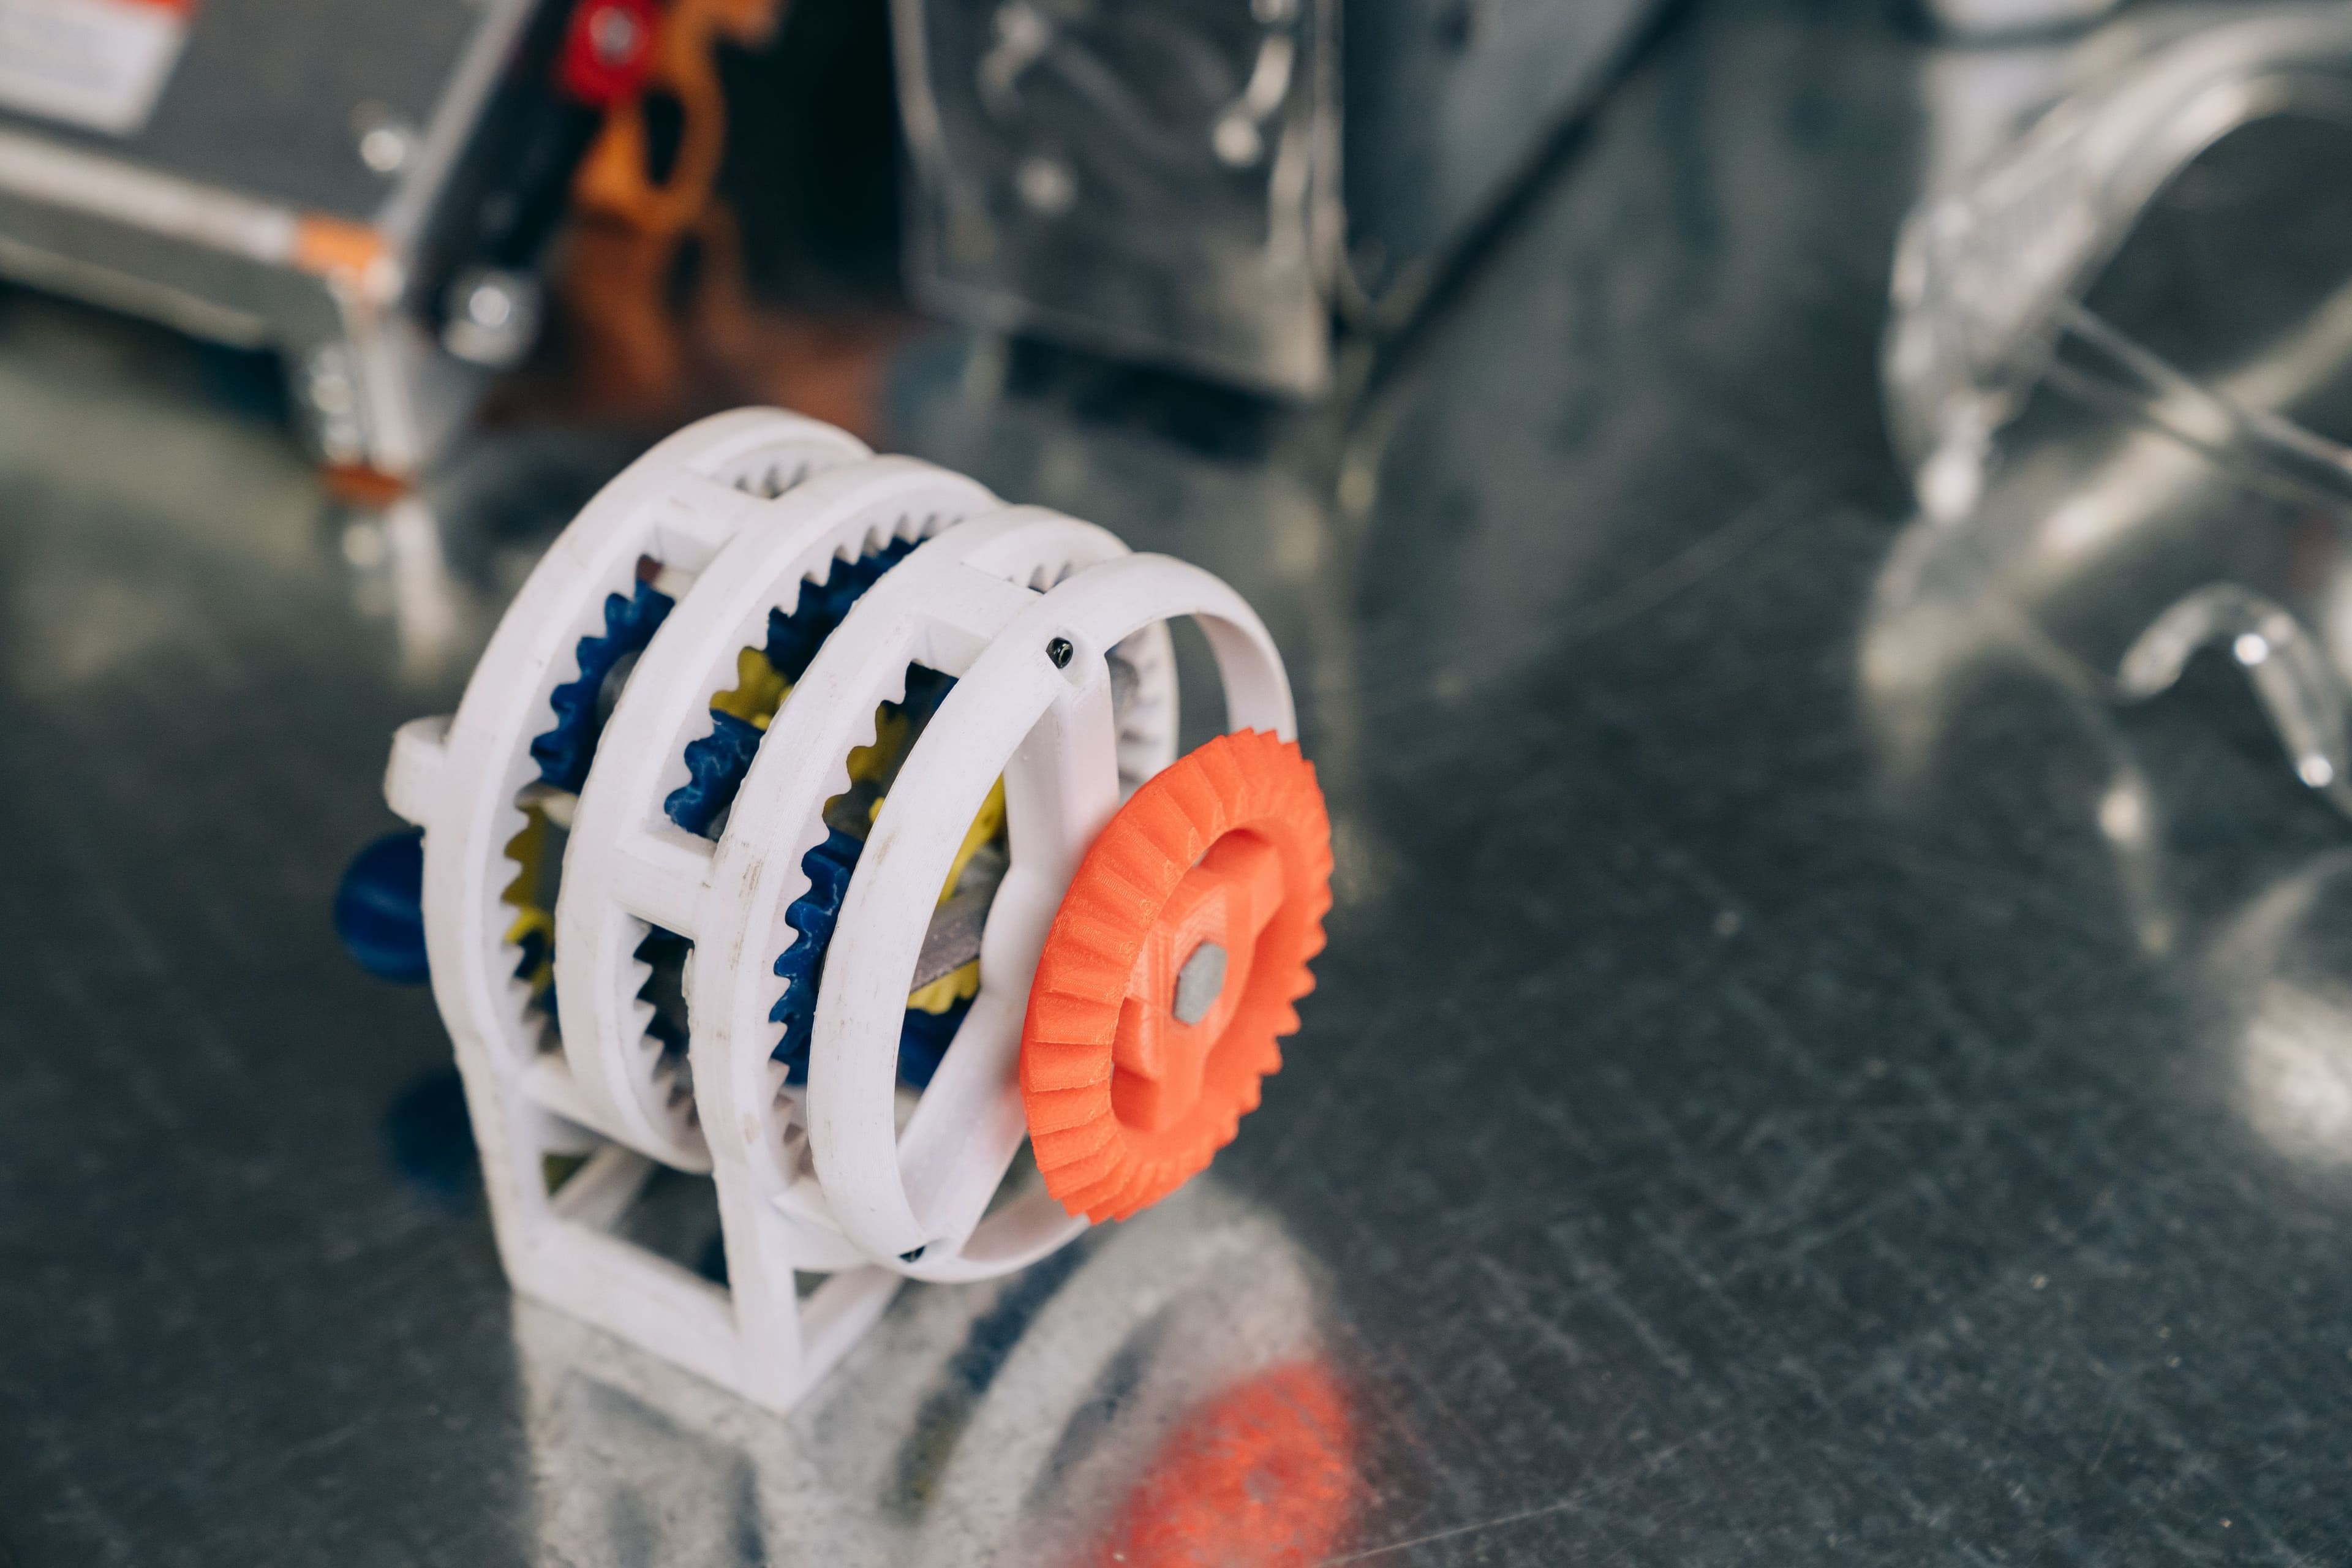
Why Consolidation Works in Powder-Bed Processes
Traditional manufacturing punishes complexity. Every undercut demands a mould slide, every internal feature another machining operation, every fastener another drilled hole and alignment step.
Part Consolidation evaluation flow
Define requirements, narrow the material and process, then verify with a consistent acceptance method.
- 1Requirements
Function, environment, quantity and risk
- 2Options
Material, process, design controls and finishing
- 3Acceptance
Dimensions, functional tests and production records
Compare the practical options
Compare material, process, design controls and finishing together—not unit price alone.
Design Considerations That Separate Success From Scrap
Consolidated parts fail in predictable ways. The first SLM manifold on almost every programme comes out with trapped powder; the first MJF consolidated bracket has a wall thickness that the datasheet said was fine but in practice warps during cool-down; the first consolidated housing has internal features no one can inspect.
| recommended practice | common mistake |
|---|---|
| Design 4 mm minimum drain/access ports for every enclosed cavity | Trust the CAD model if there is no line-of-sight for powder to escape |
| Keep internal passages above 2 mm for SLM, 3 mm for MJF | Scale down a traditional passage and assume the same flow |
| Leave critical mating faces as CNC stock with 0.5 mm to clean | Try to hit tolerance on a net-shape printed sealing surface |
| Respect the build envelope; split into two matable prints if needed | Consolidate past the build volume and pay the 2× specialty bureau rate |
| Print a coupon with the same wall thickness before the first hero part | Qualify the design straight from CAD without a wall-thickness sample |
Validate before scaling
Before scaling, verify dimensions, function and records with one controlled method across representative lots.
Pre-RFQ review: recommended practice and common mistakes
| Recommended practice | Common mistake |
|---|---|
| Document function, environment, quantity and risk | Select from a material name or machine specification alone |
| Review material, process, design controls and finishing together | Address manufacturing limits only after design freeze |
| Inspect critical dimensions and function on the first article | Scale production from visual approval alone |
| Keep material, revision and inspection records | Reuse old results after a material or process change |
- Function, environment, quantity and risk are documented
- Material, process, design controls and finishing are reviewed with the supplier
- Critical dimensions, appearance and functional acceptance are on the drawing or RFQ
- First-article or pilot-lot verification is planned
- Material, process and revision changes trigger a new review
FAQ, further reading and sources
What should be defined first for Part Consolidation?
Start with function, environment, quantity and acceptance criteria. These inputs narrow the practical options faster than naming a machine or material first.
Can typical values in this article be released directly on a drawing?
No. Use them for early comparison, then confirm the exact grade, supplier capability and first-article result.
When is the process ready to scale?
Scale only after material, process, finishing and inspection are controlled and repeatable across representative lots.
Next, explore 3D printing services, CNC machining, materials, and the related reports linked on this page.